

Crosshead Assembly, Guide Clearances & Piston Rod Stuffing Box
Master marine crosshead assemblies: oscillating pin lubrication, guide shoe clearances, stuffing box tri-zone sealing rings, and running-in protocols.
1. Operating Mechanics & Hydrodynamics of Marine Crossheads
In large two-stroke marine crosshead engines, the crosshead assembly serves as the vital kinematic junction connecting the purely reciprocating piston rod to the oscillating and rotating connecting rod. By absorbing all transverse horizontal side-thrust forces generated by connecting rod angularity, the crosshead ensures that the piston rod moves exclusively in a pure, true vertical straight line, eliminating lateral side thrust against the cylinder liner walls.
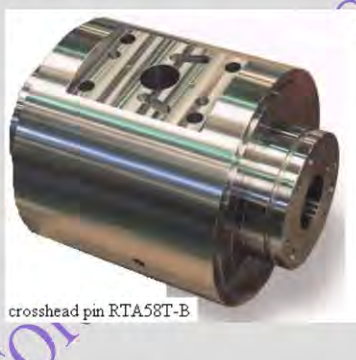
Why the Crosshead Pin is Uniquely Difficult to Lubricate
From a tribological standpoint, the crosshead pin (gudgeon pin) is universally recognized as the most severe hydrodynamic bearing application in the entire propulsion plant for three fundamental physical reasons:
- Oscillating Rather than Rotating Motion: Unlike crankshaft main and crankpin bearings that rotate continuously through 360°, the crosshead pin only oscillates through a narrow angular arc of approximately ±15° to ±20° relative to the connecting rod. The surface velocity between pin and shell is extremely low (dropping to zero velocity at each dead center), which severely limits the hydrodynamic shear wedge mechanism from dragging oil into the loaded zone.
- High, changing load near low-speed reversal: Gas and inertia forces determine the bearing load through the cycle; the loaded zone and magnitude are engine-dependent. Near dead centres the pin's oscillating surface speed becomes very low, so hydrodynamic oil-film formation is difficult exactly when substantial load may remain. This is why the maker's pressure-fed arrangement and flow monitoring matter; do not assume the load is identical throughout the cycle.
- High local bearing load: Combustion force is carried through the crosshead pin and bearing surfaces. The design load and allowable pressure are specific to the engine and bearing; cylinder firing pressure is not the same quantity as crosshead-bearing surface pressure.
Engineering Solutions: High-Pressure Booster Lubrication
To ensure an unbroken lubricating film under these punishing conditions, engine designers employ specialized hydrodynamic and hydrostatic measures:
- Crosshead pressure-fed lubrication: Depending on engine design, a separate booster circuit may raise oil pressure above the main-bearing supply so oil reaches the loaded crosshead bearing. Published engine examples include roughly 10–16 bar, but the circuit arrangement and pressure are maker-specific. The oil supply lubricates and cools the bearing; it is not a substitute for the designed clearance or specified flow.
-
Oil Supply Transmission (Articulated Arm vs. Telescopic Pipe):
- Articulated arm: a jointed pipe assembly follows the crosshead motion while maintaining the oil connection; joint and pressure details differ by maker.
- Telescopic pipe: nested stationary/moving pipes accommodate reciprocation. Inspect the actual arrangement, seals and supports in the engine manual; do not assume every design has the same valves or cushioning chambers.
- Full-Length Continuous Lower Bearing Shell: Older designs used split fork bearings. Modern engines utilize a single, continuous full-width lower bearing saddle spanning the entire bottom of the crosshead pin, drastically reducing specific load concentration.
2. Crosshead Guide Shoes, A-Frame Guides & Clearance Calibration
As the connecting rod swings through its angular arc, the oblique vector of the connecting rod thrust resolves into a horizontal force component acting athwartships. This lateral thrust is absorbed entirely by the crosshead guide shoes (slippers) sliding vertically against stationary guide bars bolted onto the transverse 'A' frames.
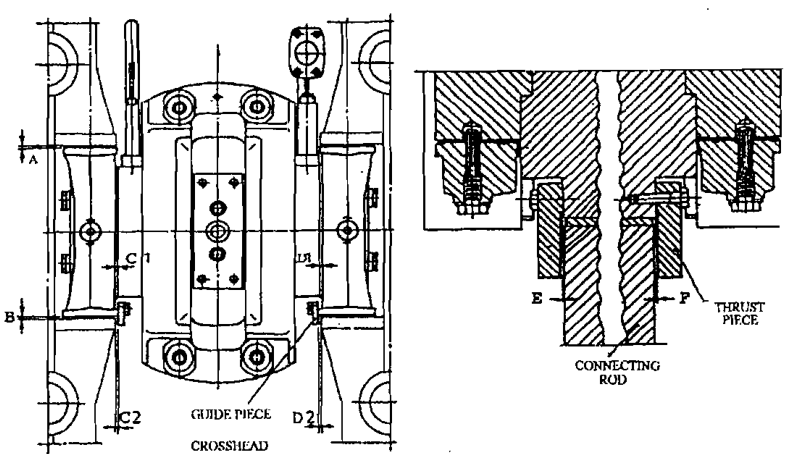
Guide Shoe Kinematics & Side Thrust Mechanics
Transverse Guide Side Thrust (Fguide) Fguide = Fpiston × tan(φ) = Fpiston × R × sin(θ)√(Lrod2 - R2sin2(θ))Guide Shoe Clearance Measurement & Tolerances
Guide shoe running clearances must be maintained within tight tolerances:
-
Athwartships (Port/Starboard) Clearance: Measured between the white metal face of the guide shoe and the cast iron guide bar using long, flexible blade feeler gauges inserted from the top, middle, and bottom of the stroke:
Engine Bore Size Design Running Clearance Maximum Permissible Wear Limit Small Bore (500–600 mm) 0.30 mm to 0.40 mm 0.65 mm Large Bore (700–950 mm) 0.40 mm to 0.50 mm 0.80 mm - Fore-and-Aft Clearance: Measured between the guide shoe side retaining gibs and the guide bar edges (typically 0.50 to 1.0 mm) to prevent mechanical binding during thermal expansion of the bedplate and frames.
- Clearance Adjustment via Shims: If athwartships clearance exceeds wear limits, the guide shoes are unbolted from the crosshead pin ends and precision ground steel shims are inserted or removed behind the shoe backing plate to restore factory running clearances.
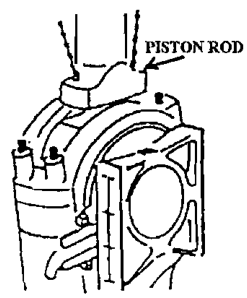
3. Piston Rod Stuffing Box: Tri-Zone Architecture & Sealing Rings
The piston rod stuffing box is the critical hermetic barrier separating two fundamentally hostile environments: the under-piston scavenge air space (containing pressurized air at 1.5–3.5 bar, hot abrasive carbon soot, unburnt fuel residues, and acidic condensed sulfuric acid) and the crankcase enclosure (containing millions of liters of pristine, highly expensive circulating system lubricating oil).
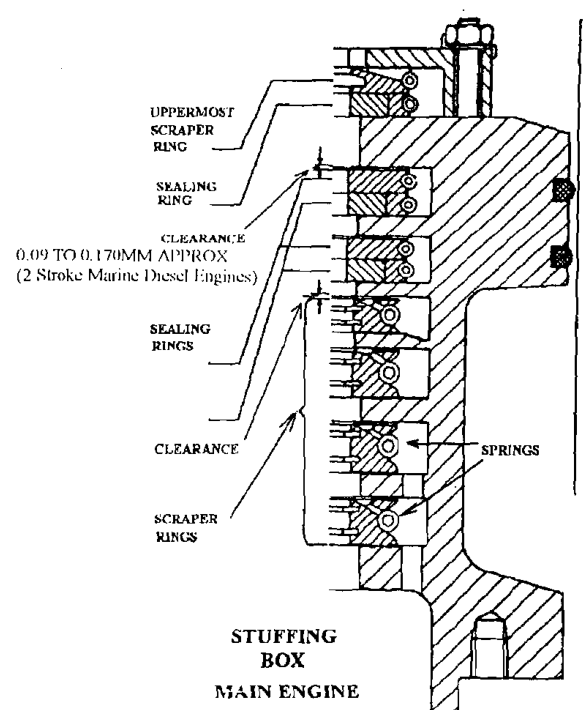
The Three Functional Sealing Zones
| Zone | Ring Pack Subassembly | Material & Design | Engineering Purpose & Destination |
|---|---|---|---|
| 1. Upper Zone (Scavenge Sealing) |
• 1 Sludge Scraper Ring • 2 to 3 Sealing Ring Sets |
Brass, lead-bronze, or special flake-graphite cast iron. 4 segments per ring with overlapping step-cut or scarf joints. | Blocks downward gas blow-by: Prevents 3.5 bar scavenge air, acidic sulfuric water, and combustion carbon from entering the crankcase. Discharges directly to the Scavenge Drain Sludge Tank. |
| 2. Middle Zone (Neutral Cofferdam) |
Atmospheric Relief Space / Cofferdam Chamber | Open annular gallery drilled through the stuffing box casing. | Diagnostic Leakage Indicator: Provides a physical pressure break. Fitted with a dedicated open drain pipe and sight glass leading to a sampling funnel. Allows engineers to instantly verify whether upper sealing rings or lower scrapers are leaking. |
| 3. Lower Zone (Crankcase Oil Scrapers) |
4 to 5 Oil Scraper Ring Sets | Fine-grain pearlitic cast iron. 3 segments per ring with ground sharp downward-facing scraper edges (lamellae). | Blocks upward oil pumping: Strips system lube oil off the descending piston rod as it enters the crankcase. Oil drains through vertical relief holes back into the Crankcase Sump / Stuffing Box Drain Tank. |
4. Segmented Ring Clearances, Wear Limits & Garter Springs
Because stuffing box rings must be installed and renewed around the continuous cylindrical piston rod without dismantling the crosshead or removing the rod from the engine, they are manufactured exclusively in interlocking segments (typically 3 or 4 segments per ring).
Butt Clearance & Gap Dynamics
When new segmented rings are fitted around a newly ground piston rod, precision butt clearances are machined into each joint:
| Ring Type | Number of Segments | Initial Butt Clearance per Joint | Total Cumulative Butt Gap | Renewal Limit |
|---|---|---|---|---|
| Upper Sealing Rings | 4 segments | 4.0 mm to 5.0 mm | 16.0 mm to 20.0 mm | Renew when gap reduces to ≤ 2.0 mm per joint. |
| Lower Oil Scrapers | 3 segments | 6.0 mm | 18.0 mm | Renew when gap reduces to ≤ 2.5 mm per joint. |
Why must there be a large butt gap? As the ring segments wear against the reciprocating rod, the garter spring pulls the segments radially inward. The butt gaps gradually close together. If the butt ends ever touch (butt gap = 0), the segments can no longer contact the rod, completely destroying the seal and allowing oil or air to gush past!
Axial (Vertical) Groove Clearances
- Measurement Method: Insert flexible blade feeler gauges between the top of the ring segment and the upper land of the stuffing box housing groove.
- Acceptance Tolerances: Standard vertical clearance is 0.07 mm to 0.12 mm (maximum in-service clearance ≤ 0.20 mm).
- Consequences of Out-of-Tolerance Clearances:
- Too Tight (< 0.05 mm): Segments bind thermally inside the groove, preventing the garter spring from holding them against the rod.
- Too Loose (> 0.20 mm): Rings flutter axially under alternating pressure cycles, rounding the knife edges and causing rapid oil pumping.
Garter Spring Mechanics & Assembly
The segments are held in uniform radial contact around the rod by an endless helical garter spring manufactured from high-tensile stainless spring steel:
- Screw-Joint Connection: One end of the spring is tapered into a narrow conical tip, while the opposite end forms an open coil. The tapered tip is screwed counter-clockwise into the female coil to form a continuous circular loop.
- Spring Tension Calibration: Over millions of engine cycles, thermal exposure causes garter springs to lose their initial pre-tension (permanent set). During every overhaul, free spring length is measured against manufacturer specifications; slack or stretched springs must be renewed immediately.
5. Piston Rod Alignment, Run-Out & Surface Tribology
The piston rod must maintain near-perfect geometric coaxiality with the engine cylinder centerline and the stuffing box bore. Even tiny angular misalignments cause severe localized side loading against the stuffing box ring segments, leading to uneven wear, ring breakage, and gland leakage.
Piston Rod Metallurgy & Surface Treatment
- Base Material: Forged low-alloy structural steel (e.g., 34CrNiMo6 or 42CrMo4), normalized and tempered for superior fatigue toughness.
- Surface Hardening: The cylindrical surface in way of the stuffing box travel is induction hardened to a depth of 3–5 mm (50–55 HRC) or electroplated with micro-cracked hard industrial chromium (hardness > 850–1000 HV).
- Surface Roughness: Super-finished to a mirror polish with Ra ≤ 0.10 to 0.20 μm. Rough surfaces act like an abrasive file, destroying bronze and cast iron scraper segments within hundreds of hours.
Piston Rod Run-Out & Coaxiality Calibration
During engine drydocking or major overhaul, piston rod straightness and alignment are verified using a dial test indicator (DTI) mounted onto the engine diaphragm plate:
Maximum Allowable Piston Rod Run-Out ΔRmax ≤ 0.05 mmCommon Piston Rod Surface Failure Modes
- Blueing / Thermal Discoloration: Bluish temper oxide colors indicate that localized frictional heating has exceeded 300°C to 400°C, typically caused by a seized crosshead guide shoe or a completely jammed stuffing box ring segment.
- Longitudinal Scoring / Grooving: Deep vertical score marks caused by hard foreign particles (cat fines from low-quality fuel or broken piston ring fragments) trapped between the rod and the bronze sealing segments.
- Corrosive Acid Etching: Cold corrosion pitting resulting from acidic sulfuric condensate dripping from the under-piston space down the rod surface.
6. Diagnostic Signatures of Stuffing Box Leaks & Overhaul Procedures
Engineers evaluate stuffing box integrity without dismantling by monitoring the quantity and chemical composition of discharge from the stuffing box drain system:
| Diagnostic Observation | Chemical / Physical Characteristic | Underlying Mechanical Failure & Operational Risk |
|---|---|---|
| Copious Black Acidic Sludge in Stuffing Box Drain | High viscosity, jet-black color, high insolubles, elevated TBN (calcium reserve), smelling of combustion products. | Upper Sealing Rings Defective: Scavenge air pressure is blowing combustion residues and unburnt cylinder oil past worn upper sealing rings into the neutral cofferdam. Risk of scavenge fire spreading down the rod. |
| Copious Clean Oil Flowing from Drain | Amber / golden brown color, normal system oil viscosity, low flash point reduction, clean clarity. | Lower Oil Scraper Rings Defective: Scraper ring knife-edges worn dull, garter springs slack, or scraper drain orifices choked with sludge. Excessive loss of crankcase system oil charge. |
| Crankcase System Oil TBN Dropping Rapidly | Laboratory oil analysis shows system oil TBN increasing or dropping with high iron/vanadium content. | Cross-Contamination: Highly alkaline cylinder oil sludge is entering the crankcase, causing system oil foaming, oxidation, and bearing chemical corrosion. |
| Hissing Sound / Blow-By at Neutral Drain Pipe | High-velocity air discharge emitting from the neutral space test cock during scavenge stroke. | Upper sealing ring segments broken or butt gaps closed completely (ring hang-up). |
Step-by-Step Stuffing Box Overhaul Procedure
- Preparation & Safety: Stop engine, engage turning gear, isolate starting air, post warning notices, stop all lube oil pumps, and open crankcase doors after cooldown.
- Dismantle Housing Halves: Modern stuffing boxes are split vertically into two halves. Remove the clamping bolts, separate the casing halves, and lower them onto the crosshead platform.
- Inspect Ring Segments & Grooves: Clean all parts in solvent. Measure butt clearances of each ring set using feeler gauges while assembled around the rod. Measure vertical groove clearances.
- Renew Ring Sets: Replace rings exhibiting rounded scraper edges, insufficient butt gap (≤ half initial value), or excessive groove play. Ensure scraper rings are installed with their sharp scraping knife edges pointing downwards toward the crankcase!
- Assemble & Verify Garter Springs: Screw garter spring ends together firmly; ensure each spring seats securely in its circumferential ring groove without twisting. Stagger the butt joints of adjacent ring tiers by 90° to prevent a continuous blow-by path.
- Bolt Housing & Torque: Fit new O-ring seals between the stuffing box flange and the diaphragm plate; bolt housing securely and torque to manufacturer specification.
7. Engine Running-In Programme for New Liners, Rings & Bearings
Following major overhaul—such as the renewal of cylinder liners, piston ring packs, crosshead bearing shells, or stuffing box rings—the newly installed components possess micro-scale surface roughness peaks (asperities). Subjecting fresh metal to full service loads immediately guarantees thermal boundary breakdown, micro-welding, scuffing, and catastrophic seizure.
A systematic Running-In Programme must be executed to progressively seat mating surfaces under controlled plastic flow:
The Two-Stage Running-In Protocol
-
Stage 1: Breaking-In Phase (Unloaded Dock Trial):
- Operate the engine uncoupled or moored alongside at Dead Slow Ahead (approx. 20%–25% RPM) for 1 to 2 hours.
- Establish unbroken hydrodynamic boundary oil films on bearings, guide shoes, and liner walls.
- Perform an immediate crankcase inspection: check bearing temperatures by hand and infrared thermometer to ensure no rapid thermal runaways have occurred.
-
Stage 2: Progressive Stepped Load Programme (Sea Trials):
The engine load is increased in disciplined increments over 48 to 72 hours:
Running-In Stage Engine Load (% MCR) Duration Operational Directives Step 1 25% to 30% MCR 4 to 6 hours Set cylinder lubricators to +50% overfeed; keep jacket water temperature moderately low (70°C–75°C) to limit thermal expansion. Step 2 50% MCR 6 to 8 hours Inspect scavenge drains and stuffing box drains; monitor cylinder exhaust temperatures for uniformity. Step 3 70% to 75% MCR 12 to 16 hours Reduce cylinder lubrication feed rate to +25% overfeed; raise jacket water to normal service level (82°C–85°C). Step 4 85% MCR (Normal Sea Load) 24 hours Verify steady-state thermal equilibrium; restore cylinder oil feed rate to standard Alpha/Pulse baseline. Step 5 100% MCR (Full Rating) 2 to 4 hours Final verification under maximum mechanical and thermal stresses; take indicator cards.
The Fuel & Lubricant Strategy During Running-In
- Cylinder Lubrication Over-Feed: For the first 100 to 200 running hours, increase cylinder oil dosage by 20% to 50% above baseline (typically 1.2 to 1.5 g/kWh) to flush away micro-abrasive wear debris.
- Controlled Corrosive Wear: During running-in on Heavy Fuel Oil, running a cylinder oil with slightly lower Total Base Number (TBN) allows controlled, mild acidic micro-etching that accelerates the flattening of cast iron asperities, preventing bore glazing.
Found a mistake, or something unclear?
Report it in a few seconds — it goes straight to the editors.
- Two-Stroke Structure — Frame, Tie Rods, Liner, Piston & Crosshead
- Marine Crankshafts — Builds, Bedplate, Chocks & Alignment
- Engine Bearings — Renewal, Crosshead to Thrust Block
- Camshaft Chain Drive, Hydraulic Tensioners & Timing Synchronisation
- Crosshead Assembly, Guide Clearances & Piston Rod Stuffing Box
- Cylinder Liner Wear, Calibration & Cold Corrosion
- Piston Crowns, Piston Rings & Thermal Mechanics
- Exhaust Valve Actuation, Air Spring Mechanics & Spindle Metallurgy
- Engine Bedplate Foundation, Holding Down Bolts & Epoxy Chocking
- Crankshaft Alignment, Web Deflections & Bearing Clearances