

Safe Engine Room Watchkeeping: UMS Certification, Physical Rounds, Automation Safeguards & Emergency Response
Master marine engine room watchkeeping: SOLAS UMS requirements, physical inspection rounds, safety slowdown/shutdown matrices, and quick-closing fuel valves.
1. Regulatory Framework: STCW Watchkeeping Principles & SOLAS UMS Mandates
The safety of a vessel, its personnel, its cargo, and the marine environment depends fundamentally on the continuous, competent operation of its propulsion machinery and auxiliary plants. Under the International Convention on Standards of Training, Certification and Watchkeeping for Seafarers (STCW Code Section A-VIII/2 Part 4-2), the Officer in Charge of an Engineering Watch (OICEW) is the Chief Engineer's direct representative, legally charged with maintaining unbroken technical vigilance, machinery efficiency, and environmental compliance.
While traditional shipping required round-the-clock manned watches in the machinery spaces, modern commercial vessels operate under Periodically Unattended Machinery Space (UMS / AUT-UMS) class notations. Under UMS operation, the engine room is completely unmanned during night hours (typically 17:00 to 08:00) and weekends, with responsibility transferred to the designated Duty Engineer via remote alarm communication networks.
SOLAS Chapter II-1 Part E: Mandatory UMS Conditions
To obtain and maintain UMS certification, a ship must prove to its Classification Society and Flag Administration that the automation plant provides a safety standard equivalent to that of a continuously manned watch:
- Bridge Propulsion Control: The Officer of the Watch (OOW) on the Navigation Bridge must have direct, independent control of propeller speed, direction of thrust, and starting/stopping without engineering intervention.
- Centralized Alarm & Monitoring System (AMS): Any abnormal operating condition must trigger immediate visual and audible alarms in the Engine Control Room (ECR), with automatic repeater alarms in the Duty Engineer’s cabin, public messrooms, and the Navigation Bridge.
- Automated Electrical Generation & Power Management (PMS): Upon sudden failure of a running generator (blackout), the standby auxiliary diesel generator must start automatically, synchronize with the switchboard, close its air circuit breaker, and re-energize essential consumers within 30 to 45 seconds. Non-essential consumers must be shed via preferential tripping.
- Comprehensive Fire Detection System: Addressable optical smoke, flame, and thermal sensors must span all machinery platforms, casing levels, and purifier flats, annunciating instantly on the Bridge and initiating general alarm escalation if not acknowledged within 2 minutes.
- Automated Bilge Level Monitoring: Machinery space bilge wells must be monitored by dual float-level transmitters. The bilge pumping arrangement must prevent dry-running of pumps and incorporate automatic lockouts preventing oily bilge water from discharging overboard.
- Air Pressure Safeguards: Main starting air receivers must maintain adequate capacity without manual intervention, equipped with automated pressure switches cycling the starting air compressors.
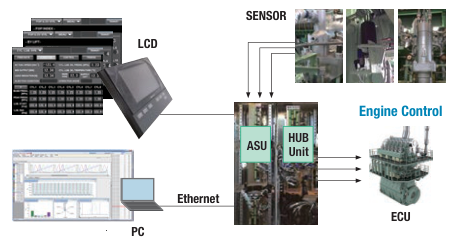
The Engineers' Alarm (Dead Man Alarm / Patrol Timer)
Whenever an engineer enters an unmanned machinery space alone outside normal working hours (e.g., attending an alarm at 02:00), their life and safety are protected by the Engineers' Safety Patrol Timer (Dead Man Alarm):
- Operation: Upon entering the machinery space, the engineer activates the patrol timer at the entrance or ECR. The timer establishes a countdown period—typically adjustable between 12 and 27 minutes.
- Reset Stations: Pushbutton reset stations are installed strategically throughout the engine room (top platform, middle platform, bottom plates, steering flat, purifier room). The engineer must press a reset button before the countdown expires.
- Escalation Sequence:
- If the timer reaches zero without a reset, an audible warning pre-alarm sounds exclusively inside the engine room for 60 seconds.
- If still unacknowledged (indicating the engineer may have slipped, fallen unconscious, suffered asphyxiation, or suffered electrical shock), the system triggers an emergency escalation alarm directly in the Navigation Bridge and in the cabins of the Chief Engineer and second engineer.
2. Sensory Vigilance & The 15-Point Physical Inspection Route
Modern automation systems monitor thousands of analog and digital data points. However, an experienced marine engineer recognizes that instruments report only what they are programmed to measure. A temperature thermocouple will read normal while hot fuel oil sprays from a loose compression fitting directly onto an uninsulated exhaust pipe flange 10 centimeters away.
Warning: The Cubicle Complacency Hazard
"Cubicle Complacency"—the dangerous habit of sitting behind the air-conditioned glass of the Engine Control Room, watching computer monitors without physically walking the plant—is a primary root cause of catastrophic shipboard machinery fires and engine write-offs. Gauges cannot smell vaporized oil. Gauges cannot see fuel atomization mist. Gauges cannot hear bearing scuffing in its earliest stages.
The 15-Point Physical Inspection Protocol
| Machinery Zone | Check Point | Sensory Method & Specific Engineering Observations |
|---|---|---|
| Top Platform (Cylinder Heads & Uptakes) | 1. Exhaust Gas Uptakes & Funnel | Sight: Check exhaust smoke color from the funnel deck or TV monitor (clear/light haze normal). Inspect expansion bellows for cracks, hot spots, or gas leakage. Listen for turbocharger surging hum. |
| 2. High-Pressure Fuel Piping | Sight & Touch: Inspect all double-walled high-pressure fuel injection pipes and trace the leak-off collector drains. Verify alarm tank float is free. Never use bare hands near pressurized fuel joints! | |
| 3. Cylinder Head Mountings | Sight & Sound: Check indicator cocks are fully closed with no combustion gas chattering. Inspect safety relief valves for signs of leakage. Check exhaust valve air spring supply pressures (6 to 7 bar). | |
| 4. Jacket Cooling De-aeration | Touch: Verify high-point air vent pipes on cylinder cover water outlets are hot, proving continuous de-aerating flow back to the expansion tank with zero vapor locks. | |
| Middle Platform (Camshaft & Scavenge Trunk) | 5. Cylinder Lubricators | Sight & Count: Observe mechanical lubricator sight-glasses or Alpha/Pulse lubricator status LEDs. Verify stroke frequency, oil level in daily tank, and delivery pressure. |
| 6. Scavenge Air Manifold | Touch & Temperature: Feel scavenge space doors for localized hot spots. Observe scavenge air manifold thermometer (< 45°C). Check non-return flap valves for chatter. | |
| 7. Under-Piston Scraper Drains | Sight: Inspect the under-piston sludge drains through the sight glasses. Flow must be lukewarm with viscous dark cylinder drain oil; black dry carbon or glowing sparks indicates active ring blow-by or impending scavenge fire. | |
| 8. Fuel Injection Pumps | Hearing & Sight: Listen for sharp, crisp fuel pump roller follower snaps. Inspect spill piping, rack teeth, and governor linkages for binding, missing split pins, or loose locknuts. | |
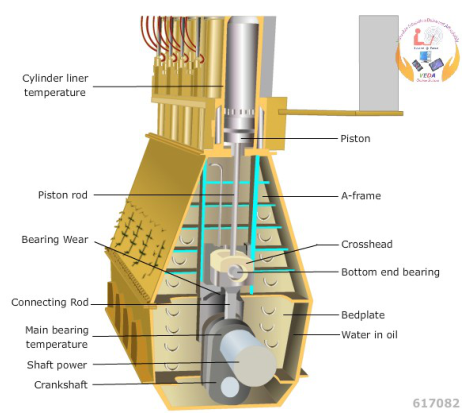
| Bottom Plates (Crankcase & Running Gear) | 9. Crankcase Doors & Relief Valves | Touch-Feel: Use the back of the hand to touch each crankcase inspection door opposite main and bottom-end bearings. All doors must exhibit uniform, warm temperature (~45°C–55°C). A localized hot door indicates bearing wipe or overheated guide shoe! Verify flame arrestor gauze is clean and free of oily rags. |
| 10. Oil Mist Detector (OMD) | Sight & Operation: Verify OMD sampling rotary valve is cycling smoothly across all sampling points. Verify zero obscuration reading and clear green healthy LED. | |
| 11. Piston Rod Stuffing Box Drains | Sight: Check sight glass collectors for stuffing box drain oil. Verify clean system oil drain return vs contaminated under-piston sludge drain separation. | |
| 12. Main Sump Level & Pressure | Sight: Verify main engine wet sump or drain tank level gauge. Verify main lube oil pressure (≥ 3.5 to 4.5 bar) and crosshead booster pressure (≥ 10 to 12 bar). | |
| Auxiliary Spaces (Purifiers, Boilers, Bilges) | 13. Fuel & Lube Purifiers | Sight & Sound: Check bowl operating water seal, clean heavy phase discharge, operating temperatures (HFO 98°C, LO 85°C), and verify sludge discharge cycle counters. |
| 14. Auxiliary Boiler & Feed System | Sight: Blow down boiler gauge glasses to confirm true water level. Check burner flame quality, steam pressure, hotwell temperature (80°C–90°C), and feed pump differential pressure. | |
| 15. Bilges & Tank Tops | Sight: Inspect all dry bilges, forward and aft cofferdams, and shaft tunnel wells. Confirm no liquid accumulation. Verify bilge alarm float sensors are unobstructed and clean. |
3. Machinery Protection: Slowdown/Shutdown Matrices & Remote Quick-Closing Valves
When operating parameters drift outside acceptable operational limits, modern propulsion automation systems execute a structured escalation ladder designed to balance machinery protection against vessel navigational safety.
The Four-Tier Protection Hierarchy
- Tier 1: Pre-Warning Alarm: Alerts watchkeepers that a parameter has exceeded standard operating envelope (e.g., Jacket water temp > 88°C).
- Tier 2: Automatic Corrective Action: Automated systems initiate corrective action without disturbing propulsion (e.g., auto-start of standby sea water pump, auto-opening of 3-way temperature mixing valve).
- Tier 3: Safety Slowdown: If parameter continues degrading, the governor reduces fuel rack index to a preset safe level (typically Dead Slow / Slow Ahead, ~40% MCR). The Navigation Bridge receives an audible alarm and a 120-second cancellation delay button to override the slowdown if navigating in restricted waters.
- Tier 4: Emergency Shutdown: If an existential mechanical danger occurs, the engine is shut down instantaneously by dumping fuel pump control oil or firing high-pressure puncture valves. Emergency shutdowns cannot be overridden from the bridge (except under specialized emergency run modes where permitted by flag administration).
Safety Slowdown vs. Emergency Shutdown Trigger Matrix
| Action Level | Triggering Monitored Parameter | Standard Trip Setpoint | Bridge Override Permitted? |
|---|---|---|---|
| SAFETY SLOWDOWN (Reduces engine to Slow Ahead ~40% load) |
High Jacket Water Outlet Temperature | > 92°C to 95°C | YES (Bridge Override button resets timer) |
| High Cylinder Exhaust Gas Temperature | > 460°C or ΔT > 50°C across units | YES | |
| Low Piston Cooling Oil Pressure / Flow | < 1.8 bar / loss of return flow | YES | |
| High Thrust Bearing Pad Temperature | > 75°C to 80°C | YES | |
| Scavenge Air Trunk Temperature | > 80°C to 90°C | YES | |
| EMERGENCY SHUTDOWN (Fuel slammed to ZERO within < 1.5s) |
Low-Low Main Lubricating Oil Pressure | < 1.2 to 1.5 bar at main bearing rail | STRICTLY NO (Hardware Interlock) |
| Engine Overspeed Trip | 110% to 115% of rated MCR RPM | STRICTLY NO (Mechanical / SIL-3 trip) | |
| High-High Oil Mist Detector (Crankcase) | > 2.5% to 3.0% opacity (≥ 2.0 mg/L) | STRICTLY NO (Crankcase protection) | |
| Manual Emergency Stop Pushbutton | Bridge, ECR, Local Stand, Fire Station | STRICTLY NO (Manual emergency trip) |
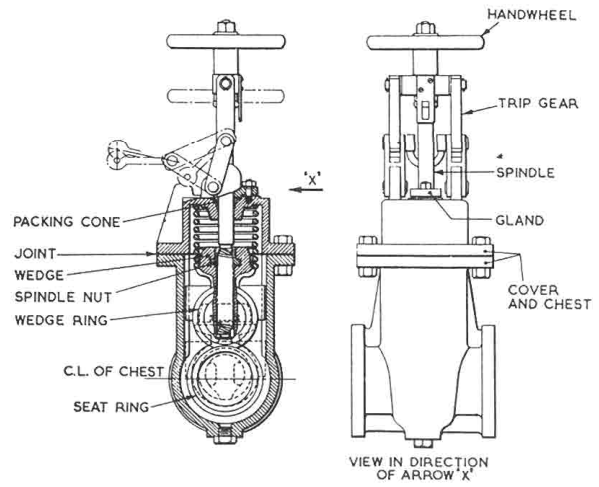
Remote Quick-Closing Valves (QCVs) on Oil Tanks
Under SOLAS Chapter II-2 Regulation 4, every oil fuel and lubricating oil tank located within machinery spaces with a capacity exceeding 500 liters must be fitted with valves capable of being closed remotely from outside the compartment in the event of an engine room fire.
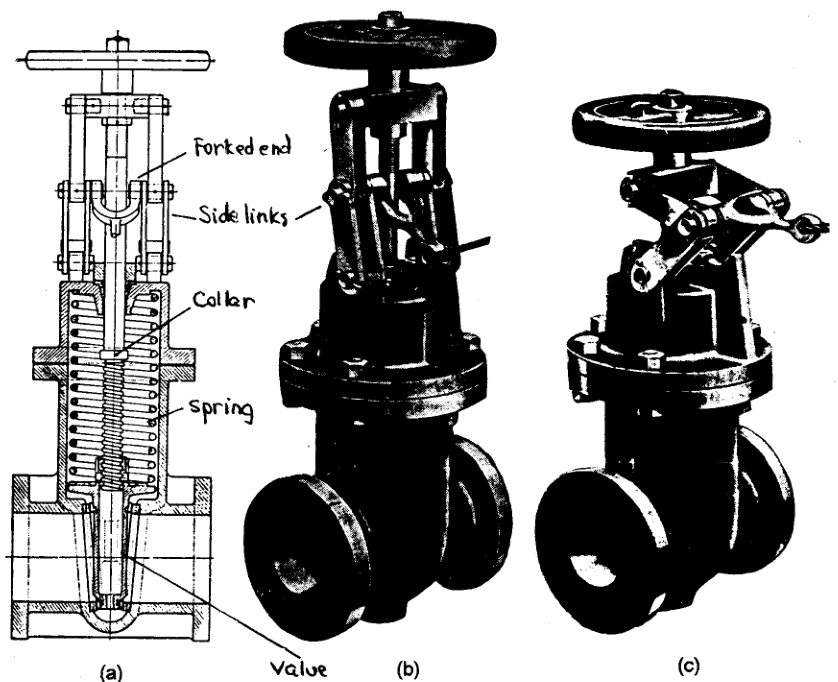
- Instanter Valve Mechanics: The valve is held open against a powerful helical compression spring by a mechanical toggle or latch pin. When tripped, the latch releases, allowing the heavy spring to slam the internal valve disc down onto its seat, cutting off gravity fuel flow.
- Actuation Modes:
- Pneumatic Tripping: Dedicated 7 to 10 bar compressed air bottles located in the Fire Control Station discharge air via directional push-pull valves directly to small release cylinders mounted on each valve body.
- Mechanical Wire-Pull (Morse Cable): Stainless steel pull cables run through conduit pipes from external pull-boxes directly to the mechanical trip triggers.
- Testing Requirements: Classification societies require routine, documented testing of all quick-closing valves (typically every 3 to 6 months in port). Valves must be tripped remotely, verified visually shut on tank bottoms, and manually reset using their handwheels.
4. Human Error Prevention: The Overhaul Pitfall Matrix & Tool Accountability
Investigations by maritime accident investigation branches (MAIB, NTSB, BSU) consistently reveal that over 80% of major marine machinery disasters are precipitated by human maintenance error rather than spontaneous metallurgical fatigue. Modern marine engineering demands rigid quality assurance procedures during major maintenance.
Danger: Six Classic Overhaul Pitfalls That Destroy Engines
| Fatal Overhaul Mistake | Disastrous Consequence | Mandatory Prevention Protocol |
|---|---|---|
| 1. Cleaning Rag Left Inside Crankcase | The loose cotton rag migrates into the bedplate sump, reaches the lube oil suction strum, and blinds the mesh. Lubricating oil pressure collapses, resulting in multiple spun main bearing shells and crankcase explosion. | Strict Tool & Cloth Count: Maintain a signed "Crankcase Entry Logsheet". Count every single wiping rag and socket wrench entering and exiting. Final inspection by Chief Engineer before sealing doors. |
| 2. Connecting Rod Bolts Under-Torqued or Yielded | Bottom-end bolts subjected to insufficient pre-stretch suffer alternating high-cycle fatigue, shearing off during sea passage. The freed connecting rod acts as a massive flail, punching through the cast iron bedplate and wrecking the crankshaft. | Hydraulic Bolt Stretch Measurement: Never guess bolt torque! Use calibrated hydraulic tensioners. Measure physical bolt elongation with a micrometer or depth gauge against maker’s elastic stretch datum (ΔL). |
| 3. Solid Gasket Fitted Without Punching Center Hole | An engineer cuts a new gasket from jointing paper, punches bolt holes, but forgets to punch the central fluid passage hole. Lube oil or cooling water is completely blocked, burning out bearings or seizing pistons within 5 minutes. | The Light Test: Hold every newly fabricated gasket up against a bright light bulb alongside the component flange before bolting up. Verify 100% passage alignment. |
| 4. Skipping Injector Test Bench Calibration | Refitting overhauled fuel injectors without testing on the hydraulic hand bench. An injector with an eroded nozzle or stuck needle dribbles fuel, creating local hot spots, burning a hole through the piston crown. | Mandatory 4-Point Pop Test: Pop test every injector: verify opening pressure (±5 bar), atomization cone uniformity, crisp needle chatter, and 10-second drip-tightness under test pressure. |
| 5. Misuse of Hydraulic Tensioning Tools | Applying excessive hydraulic pressure (> specified bar) yields tie-bolt or cylinder head studs beyond their elastic limit, causing permanent plastic elongation or stripped threads. | Certified Gauges & Staged Pressurization: Verify pump calibration certificate. Increase pressure in stages; never exceed maximum allowable pressure on data plates. |
| 6. Painted or Lagged Expansion Joints & Valve Spindles | Painting over safety relief valve spindles or lagging over expansion bellows restricts thermal movement, causing pipe rupture or relief valve failure during overpressure. | Visual Masking: Mask all valve spindles, relief valve springs, and indicator linkages with tape before painting machinery spaces. |
Tool Accountability & Closed-Compartment Discipline
Before any crankcase door, scavenge inspection door, or gearcase cover is bolted shut:
- The work site is swept with powerful industrial magnets to retrieve loose washers, split pins, or wire lock clippings.
- The Chief Engineer and First Assistant Engineer perform an independent Four-Eye Inspection with explosion-proof torches, physically checking oil return galleries, balance weight lock-plates, and crosshead slipper clearances.
- The official "Permit to Close Machinery Compartment" is signed, certifying zero foreign objects remain inside.
5. Engine Logbook Data Trending: Early Detection of Thermodynamic Decay
The Engine Room Daily Logbook is not merely an administrative record for company auditors; it is a vital diagnostic instrument. A single set of logged numbers provides an instantaneous snapshot, but plotting data trends over 30 to 90 days reveals progressive mechanical and thermal decay long before automated alarms are triggered.
Key Performance Parameters & Trending Significance
| Logged Parameter | Normal Operational Range | Insidious Trending Pattern | Engineering Diagnosis |
|---|---|---|---|
| Exhaust Gas Temperature (°C) | 320°C to 380°C (balanced within ±15°C) | Single cylinder temperature slowly climbing +30°C over two weeks with fixed fuel rack. | Fouled or dripping fuel injector, leaking exhaust valve spindle, or early afterburning in that unit. |
| Scavenge Air Pressure (bar) & Cooler ΔP | 1.8 to 2.5 bar at 85% MCR; Cooler ΔP ≤ 100 mm WC | Scavenge pressure dropping; cooler air-side differential pressure (ΔP) steadily climbing from 50 to 180 mm WC. | Heavy fouling of charge air cooler fin surfaces with oily dust. Requires chemical foam cleaning in port. |
| Turbocharger RPM & Exhaust ΔT | 12,000 to 18,000 RPM; ΔT across turbine ~80°C–120°C | Turbocharger RPM dropping at constant engine load; exhaust temperature into turbine rising. | Turbine nozzle ring and blade fouling with carbon deposits, or turbine labyrinth air seal erosion. |
| Cylinder Lubricating Oil Specific Feed Rate | 0.6 to 1.2 g/kWh (calculated daily) | Lubricator daily tank consumption dropping despite steady engine operating hours. | Faulty lubricator feed pump, air locked dosing unit, or stripped drive gear on mechanical lubricator. |
| Jacket Cooling Water Temperature Differential (ΔT) | ΔT across engine: 10°C to 12°C (In: ~78°C, Out: ~88°C) | ΔT across one specific cylinder widening to 18°C with normal water flow. | Severe scale formation or calcium carbonate encrustation inside cylinder liner cooling bores, restricting heat transfer. |
Specific Cylinder Oil Consumption Formula
Every sea watch must calculate and verify specific cylinder oil consumption:
Where:
- V24h: 24-hour cylinder oil consumed (m3 or Liters × 10-3)
- ρ: Cylinder oil density (typically 0.92 to 0.94 kg/L)
- P: Average engine brake power output (kW)
6. MEO Class 1 & Class 2 Examination Technical Analyses
Maritime Examiner Oral Assessment Standards
Questions on watchkeeping standards, UMS certification requirements, and emergency response procedures are primary testing grounds in MEO Class 4, Class 2, and Class 1 oral examinations. Surveyors evaluate whether the candidate demonstrates an uncompromised safety culture, legal regulatory knowledge, and disciplined technical leadership.
Q1: Outline the mandatory automated systems and safety conditions required under SOLAS Chapter II-1 Part E for a vessel to operate with an Unmanned Machinery Space (UMS).
Model Engineering Answer:
To satisfy SOLAS II-1 Part E and class AUT-UMS notation, the machinery installation must ensure safety equivalent to a continuous watch:
- Bridge Propulsion Remote Control: The bridge officer must have direct command of propulsion speed and direction via a single lever, with automatic start sequencing, load-up programs, and barred speed range lockouts.
- Centralized Alarm Monitoring System (AMS): Must detect and display all abnormal machinery parameters in the ECR, with automatic duty-engineer cabin call systems, messroom alarm repeaters, and bridge warning repeaters.
- Automated Power Management (PMS): Automatic starting, synchronizing, load sharing, and breaker closing of a standby generator upon failure of a running unit within 30 to 45 seconds, accompanied by preferential tripping of non-essential loads.
- Addressable Fire Detection Network: Comprehensive coverage of all machinery zones with dual-sensor detection (smoke and flame/heat), triggering bridge alarms and general ship alarm escalation within 2 minutes if unacknowledged.
- Automated Bilge System: Multiple level switches in all bilge wells with high-level alarms, autonomous bilge water level monitoring, and oily water separator overboard discharge lockouts.
- Emergency Power & Steering Redundancy: Autonomous emergency generator starting within 45 seconds under dead-ship conditions, and automatic steering gear power restoration.
Q2: Explain the operational differences between an Engine Safety Slowdown and an Emergency Shutdown. What are the bridge override protocols?
Model Engineering Answer:
Safety Slowdown:
A safety slowdown is initiated when a non-fatal, yet severe thermodynamic or thermal overload occurs (e.g., high exhaust temperature, high jacket water temperature, low piston cooling flow, high thrust bearing temp). The governor automatically reduces the engine fuel index to ~40% MCR (Slow Ahead) to reduce heat input while preserving vessel steerage and maneuverability.
Bridge Override: Because slowing down in a narrow shipping lane or congested fairway could cause collision or grounding, SOLAS permits a Bridge Slowdown Override. When a slowdown is triggered, an audible warning sounds on the bridge with a 120-second countdown. The watch officer can cancel the slowdown by pressing the "Slowdown Reset / Override" button, maintaining speed at their own discretion.
Emergency Shutdown:
An emergency shutdown is initiated exclusively by catastrophic structural or safety threats: low-low main bearing lube oil pressure (< 1.2 bar), mechanical/electronic overspeed (115% MCR), crankcase high oil mist (> 2.5% opacity), or manual E-stop pushbuttons. The automation system instantly dumps fuel pump rack control air or triggers high-pressure puncture valves, halting fuel delivery in less than 1.5 seconds.
No Override: Emergency shutdowns cannot be overridden from the bridge because permitting an engine to run without oil pressure or during an overspeed condition would cause catastrophic crankcase explosion or structural breakup.
Q3: Describe the operating mechanism of an Instanter Quick-Closing Valve (QCV) fitted on heavy fuel oil service tanks. How is it routinely tested by marine engineers?
Model Engineering Answer:
Operating Mechanism:
The Howden Instanter quick-closing valve is an inverted spring-loaded globe valve mounted directly at the tank bottom suction flange. A heavy internal helical spring constantly biases the valve spindle toward the shut position. The valve is held in the open position by a mechanical trip catch or toggle latch mechanism.
When emergency release is initiated from outside the engine room (via a pneumatic air pulse or a steel wire pull cable), the latch is disengaged. The powerful spring instantly snaps the valve disc onto its seat, overcoming hydraulic head pressure and isolating fuel flow in milliseconds.
Routine Testing Protocol:
- Testing is conducted in port with the vessel moored safely. Ensure affected engines or boilers are running on alternative tanks or temporarily secured.
- Go to the Fire Control Station outside the machinery space. Activate the remote quick-closing release cabinet (fire pneumatic bank or wire pull handle).
- Enter the engine room and verify that the valve indicator pointer on the tank bottom has visibly shifted to the SHUT position.
- Verify that the fuel supply pressure gauge downstream of the tank drops to zero.
- To reset, turn the valve handwheel fully clockwise to re-engage the internal latch catch against spring tension, then open the handwheel back to the open running position. Log the test in the Official Engine Logbook.
Q4: How does the Engineers' Safety Patrol Timer (Dead Man Alarm) function, and why is it mandatory during UMS hours?
Model Engineering Answer:
The Engineers' Safety Patrol Alarm protects an engineer working unaccompanied in an unmanned engine room outside regular day-work hours.
Function:
- Upon entry, the duty engineer starts the timer at the entrance or ECR (countdown set between 12 and 27 minutes).
- Reset pushbuttons are located across all machinery platforms. The engineer must depress a reset button before the time interval expires.
- If the timer reaches zero, a local pre-warning buzzer sounds for 60 seconds inside the engine room, allowing the engineer to press the nearest reset.
- If the pre-warning is not acknowledged within 60 seconds (indicating incapacitation due to falls, burns, gas asphyxiation, or electrical shock), the alarm escalates instantly, sounding loud sirens on the Navigation Bridge and in the cabins of the Chief Engineer and other engineering officers. The bridge team immediately dispatches a rescue team to the machinery space.
Q5: During a sea watch, you observe that exhaust gas temperatures across all cylinders are steadily creeping upward, while charge air cooler air-side differential pressure (ΔP) is rising. What is the diagnosis and required action?
Model Engineering Answer:
Engineering Diagnosis:
The simultaneous rise in charge air cooler air-side differential pressure (ΔP) and engine exhaust temperatures indicates severe fouling of the charge air cooler fin block on the air side.
- Oily airborne mist drawn from the machinery space by the turbocharger compressor mixes with atmospheric dust, baking onto the cooling tube fins.
- This restricts airflow passage (raising ΔP beyond the 100 mm WC allowable limit), throttling scavenge air mass flow into the cylinders.
- The resulting lower air-fuel ratio (λ) causes oxygen starvation, prolonging combustion into the expansion stroke (afterburning), driving exhaust temperatures up across all units.
Corrective Action:
- Verify that auxiliary scavenge blowers cut in if scavenge pressure drops significantly.
- Inject approved air cooler cleaning chemical solution using the in-service pneumatic spray system while running at reduced load (if permitted by maker).
- At the next port of call, open the air cooler inspection doors and perform thorough chemical soaking and low-pressure hot-water wash of the tube nest fin banks.
- Check turbocharger air intake filter panels and renew dirty filter mats.
Q6: Detail the procedure and legal responsibilities when handing over an engineering watch at sea in a manned engine room.
Model Engineering Answer:
Under STCW Section A-VIII/2, the relieving officer must not take over the watch until they have personally inspected the machinery spaces and satisfied themselves that all plant is operating normally:
- Reliever Pre-Conditions: The relieving officer must be fully awake, alert, unimpaired by fatigue or alcohol, and adjusted to machinery noise and lighting. If the relieving officer appears unfit, the watchkeeper must refuse handover and notify the Chief Engineer.
- Joint Walk-Through Inspection: The relieving engineer conducts a physical round from top to bottom plates, checking running gear, oil levels, bilge dry states, exhaust temperatures, and purifier operating points.
- Verbal Briefing in ECR: The outgoing watchkeeper briefs the reliever on:
- Standing orders from the Chief Engineer and bridge navigation status (speed orders, shallow waters, restricted visibility).
- Machinery running status, running maintenance in progress, and work permits active (hot work, enclosed space entry).
- Tank transfers taking place (bilge, sludge, or fuel bunker transfers).
- Equipment out of service, bypassed alarms, or tagged-out machinery.
- Logbook Formal Handover: The outgoing officer signs the logbook; the relieving officer counter-signs, formally accepting legal responsibility for the engineering watch.
Standards & sources referenced
- SOLAS: International standards for the safety of life at sea.
- STCW: International standards for seafarer training, certification and watchkeeping.
- Conventions index
Practise this in the question bank
- Engine Room - General — 57 questions
Found a mistake, or something unclear?
Report it in a few seconds — it goes straight to the editors.
- Safe Engine Room Watchkeeping: UMS Certification, Physical Rounds, Automation Safeguards & Emergency Response
- Engine Protections, Vibration Watch & Performance Curves
- Marine Diesel Engine Starting & Running Troubles: Fault Trees, Knock Diagnosis & Emergency Response
- Crankcase Explosions, Oil Mist Detectors & Relief Valves
- Scavenge Fires, Trunk Safety & Relief Devices