Troubleshooting the Sewage Plant — Ten Faults, Cause by Cause
Sewage plant troubleshooting: black effluent and odour from anaerobic conditions, dead bacteria colonies, grease ingress and float switch faults.
1. Master symptom table
Warning: Operating rule
The maker's manual and the PMS override. Do not run a plant whose air supply has failed. Anaerobic activity in a confined space produces flammable and toxic gas.
Use this as the first pass; the numbered sections below give the reasoning.
| Symptom | Most likely cause | Section |
|---|---|---|
| Offensive odour, black effluent, corrosion | Anaerobic conditions — air supply failed, plant bypassed, or sludge left too long in the settling tank | 2.1 |
| Plant not treating after a long shutdown | Bacteria colony dead | 2.2 |
| Sudden loss of treatment with no mechanical fault | Change of flushing liquid, drastic temperature change, or excess cleaning agents | 2.3 |
| No treatment at all, effluent foul | Oil or grease has entered the system | 2.4 |
| Blower failure | Mechanical failure | 2.5 |
| Aerator blockage | Dirty air — the diffuser is porous material | 2.6 |
| Excess sludge, reduced efficiency | Normal accumulation of inert residue | 2.7 |
| Discharge pump not starting, or running continuously | Float switch fault | 2.8 |
| Settling tank going septic | Sludge not being returned | 2.9 |
| Holding tank corrosion and gas | Anaerobic breakdown in the tank | 2.10 |
2. The faults in detail
2.1 Offensive odour, black effluent, corrosion
Cause. Anaerobic conditions. The symptoms are the classic signature of the anaerobic process: black, turgid water, hydrogen sulphide and methane, and corrosion of the tank. The causes are all variations on a single theme — the oxygen is not getting to where the bacteria are:
- the air supply has failed, so the aeration chamber has gone anaerobic;
- the plant has been bypassed, so sewage is passing through untreated;
- sludge has been left too long in the settling tank, where there is no oxygen by design.
Action. Restore the air supply, recycle the sludge continuously, and desludge. Then establish which of the three causes applied, because they need different follow-up.
This is the fault to treat as urgent. Once the plant is anaerobic it is producing flammable and toxic gas in a confined space, as well as not treating anything.
2.2 The plant is not treating after a long shutdown
Cause. The bacteria colony is dead. A sewage plant is a living system, and shutting it down kills it in the same way that shutting down a boiler lets the fire go out.
Action. Restart the plant and allow 5 to 14 days for a new colony to establish. There is no faster route — the extended aeration period is what grows the colony. Then keep the plant running at all times.
The 5 to 14 day figure is the reason this is worth preventing rather than curing. A ship with a dead plant on a ten-day voyage has no treatment capacity for the whole voyage.
2.3 Sudden loss of treatment with no mechanical fault
Cause. Something has changed the bacteria's environment:
- a change of flushing liquid — for example sea water to fresh water, which changes the chemistry of the incoming sewage;
- a drastic change of temperature;
- excess lavatory cleaning agents, which are designed to kill bacteria and do not distinguish between the ones in the bowl and the ones in the tank.
Action. Restore normal conditions and allow several days for regeneration. Then find the source of the change — usually a cleaning product or a change in the ship's water supply.
2.4 No treatment at all, effluent foul
Cause. Oil or grease has entered the system, and it kills the bacteria. This is the single most common cause of a dead plant, and the source is usually galley grease or a machinery space leak finding its way into the sewage system.
Action. Find and stop the source first — there is no point re-establishing a colony while the cause is still present. Then the plant must be re-established, which means the 5 to 14 day regrowth period.
2.5 Blower failure
Cause. Mechanical failure of the aeration blower.
Action. Switch to the stand-by blower, and keep it in working order — a stand-by blower that will not start is not a stand-by. Why the equipment list specifies two blowers and two discharge pumps is in The Sewage Treatment Plant, section 7.
The urgency is that the aeration chamber starts going anaerobic as soon as the air stops. Changeover should be immediate.
2.6 Aerator blockage
Cause. Dirty air. The diffuser is of porous material, and porous material blocks. If the air supply carries dust, oil carry-over from the blower, or moisture, the diffuser closes up.
Action. Supply clean air, and clean or renew the diffuser. The aerators are removable through the side or end of the tank for replacement — this is a deliberate design provision for exactly this fault.
2.7 Excess sludge, reduced efficiency
Cause. The normal accumulation of inert residue from the digestion process. The aeration volume available falls as the sludge volume rises, so treatment efficiency falls with it.
Action. Desludge about three-monthly — pump out about three quarters of the aeration tank contents and refill with clean water. Why three quarters and not the whole tank is in The Sewage Treatment Plant, section 6.
2.8 Discharge pump not starting, or running continuously
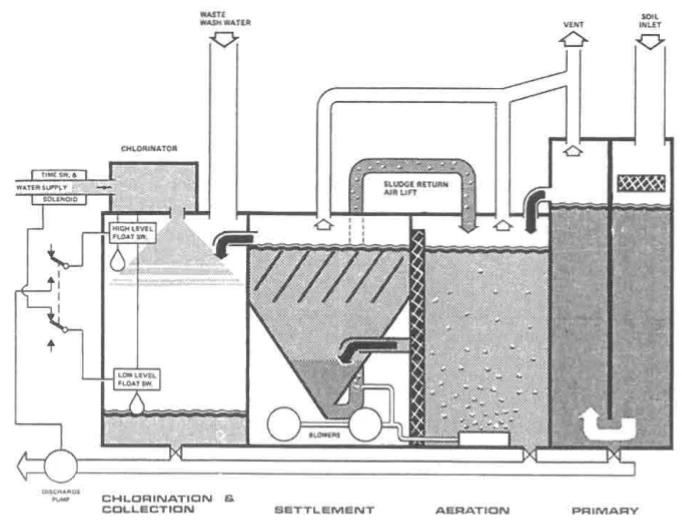
Cause. Float switch fault. Two float switches in the final section control the discharge pump — the top one starts it as the tank fills, the low level one stops it. A stuck switch produces either a pump that never runs or a pump that never stops.
Action. Check both float switches. Note that the low level switch also triggers the chlorinator dosing through the solenoid valve, so a fault there affects disinfection as well as discharge.
2.9 Settling tank going septic
Cause. The sludge is not being returned. The settling chamber is unaerated by design, so activated sludge sitting in it goes anaerobic within a short time.
Action. Check the air lift returning activated sludge to the aeration tank. A blocked air lift is the usual cause.
2.10 Holding tank corrosion and gas
Cause. Anaerobic breakdown in the tank. A plain holding tank has no oxygen in it, so putrefaction is inevitable and its products are corrosive as well as dangerous.
Action. Check the vent and the flame trap; verify the integrity of the coating; and reduce the retention time by discharging at the earliest lawful opportunity.
Found a mistake, or something unclear?
Report it in a few seconds — it goes straight to the editors.
- What Sewage Is — the Definition, the Daily Volumes, and Why It Must Be Treated
- Aerobic and Anaerobic Breakdown — Why the Colony Dies and How Long Recovery Takes
- Where Sewage May Be Discharged — the 3 Mile and 12 Mile Rules
- The Sewage Treatment Plant — Aeration, Settling and Chlorination
- Retention, Holding and Zero-Discharge Systems — Holding Tanks, Vacuum Toilets and Elsan
- Effluent Quality — BOD, Suspended Solids and Coliform Count
- Sludge Disposal — Overboard at Sea, Sullage Tank, or Incinerator
- Troubleshooting the Sewage Plant — Ten Faults, Cause by Cause
- Maintenance of the Sewage Plant — Desludging, Aeration and the Daily Checks
- Safety on the Sewage Plant — Gas Hazards and Enclosed Space Entry