Marine Fuel Injectors — Atomisation Dynamics, Slide Valves & The Seven Workshop Bench Tests
Master marine fuel injectors: differential needle lift, atomisation vs penetration, slide valve sac volume, 7 workshop bench tests, and overhaul procedures.
1. The Fuel Injection Task: Atomisation Physics, Penetration & Droplet Size
The marine fuel injector (fuel valve) is the final metering and atomizing element in the combustion chain. When the high-pressure fuel pump delivers a fuel charge at 300 to 1,200 bar, the injector must transform this solid column of viscous liquid into a highly dispersed aerosol mist composed of millions of microscopic fuel droplets.
In a large two-stroke engine running at 100 RPM, the entire injection event transpires in approximately 25 to 35 milliseconds. Within this microscopic window, the fuel spray must accomplish three simultaneous physical objectives:
- Rapid Atomisation: Break the fuel jet into microscopic droplets with a Sauter Mean Diameter (SMD / D32) of 10 to 25 μm, maximizing surface-area-to-volume ratio to accelerate heat transfer, vaporization, and chemical auto-ignition.
- Sufficient Kinetic Penetration: Impart enough kinetic momentum to droplets so they can penetrate deep into the dense, turbulent combustion air charge (compressed to 35–45 bar at 600°C) without stagnating near the nozzle tip.
- Combustion Space Trajectory: Direct the multi-hole spray cones evenly throughout the swirling scavenge air envelope to achieve complete oxygen utilization without allowing liquid fuel droplets to impinge onto the cylinder liner wall or piston crown.
The Fundamental Compromise: Atomisation vs Penetration
Marine engine combustion engineers face a classical aerodynamic conflict between atomisation quality and spray penetration:
Droplet Weber Number & Aerodynamic Breakup
Where ρair is the dense air density, Vrel is the relative velocity between fuel jet and air, and σfuel is the fuel surface tension. When the Weber number exceeds a critical threshold (~12 to 14), aerodynamic drag forces overcome surface tension, shattering the jet into fine mist.
| Spray Parameter | Physical Consequence of Deficiency | Physical Consequence of Excess |
|---|---|---|
| Atomisation (Droplet Fineness) | Too Coarse: Droplet diameter exceeds 40 μm; vaporization is sluggish; delayed combustion causes prolonged afterburning, high exhaust temperatures, black smoke, and severe unburned carbon deposits. | Too Fine: Droplets lack kinetic momentum; they decelerate within inches of the nozzle tip, creating an oxygen-starved rich core around the injector, leaving peripheral air unutilized. |
| Penetration (Spray Reach) | Under-Penetration: Fuel fails to mix with peripheral air; lower mean effective pressure (MIP) and elevated Specific Fuel Oil Consumption (SFOC). | Over-Penetration: High-velocity liquid droplets strike the cylinder liner running surface, washing away the alkaline cylinder lubricating oil film, causing liner scuffing, micro-seizure, and catastrophic crown burning! |
2. Mechanical Construction, Metallurgy & Differential Area Lifting Physics
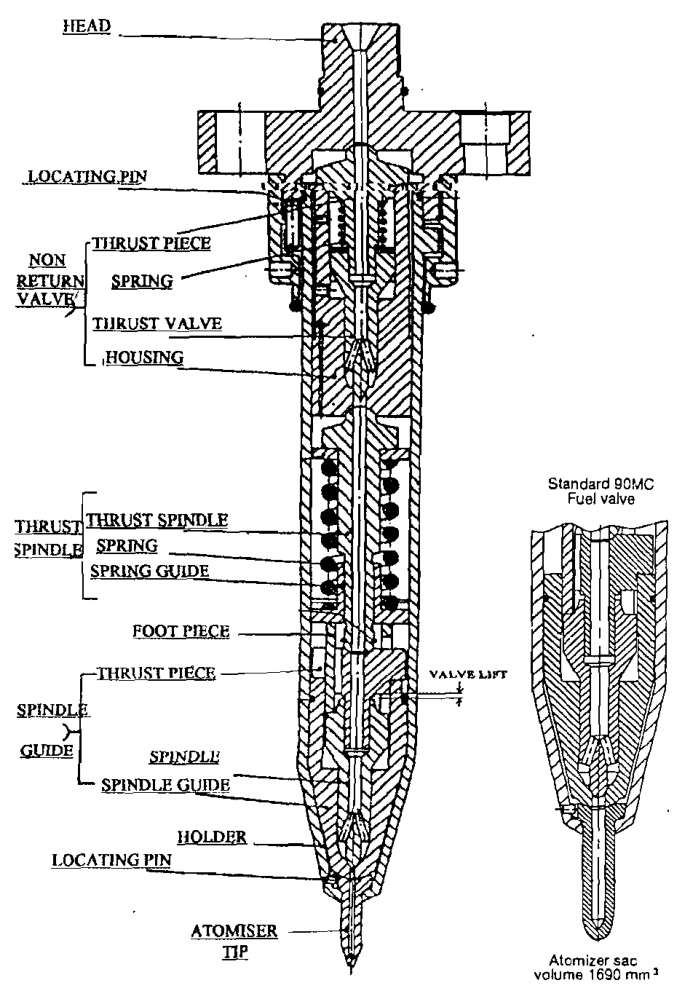
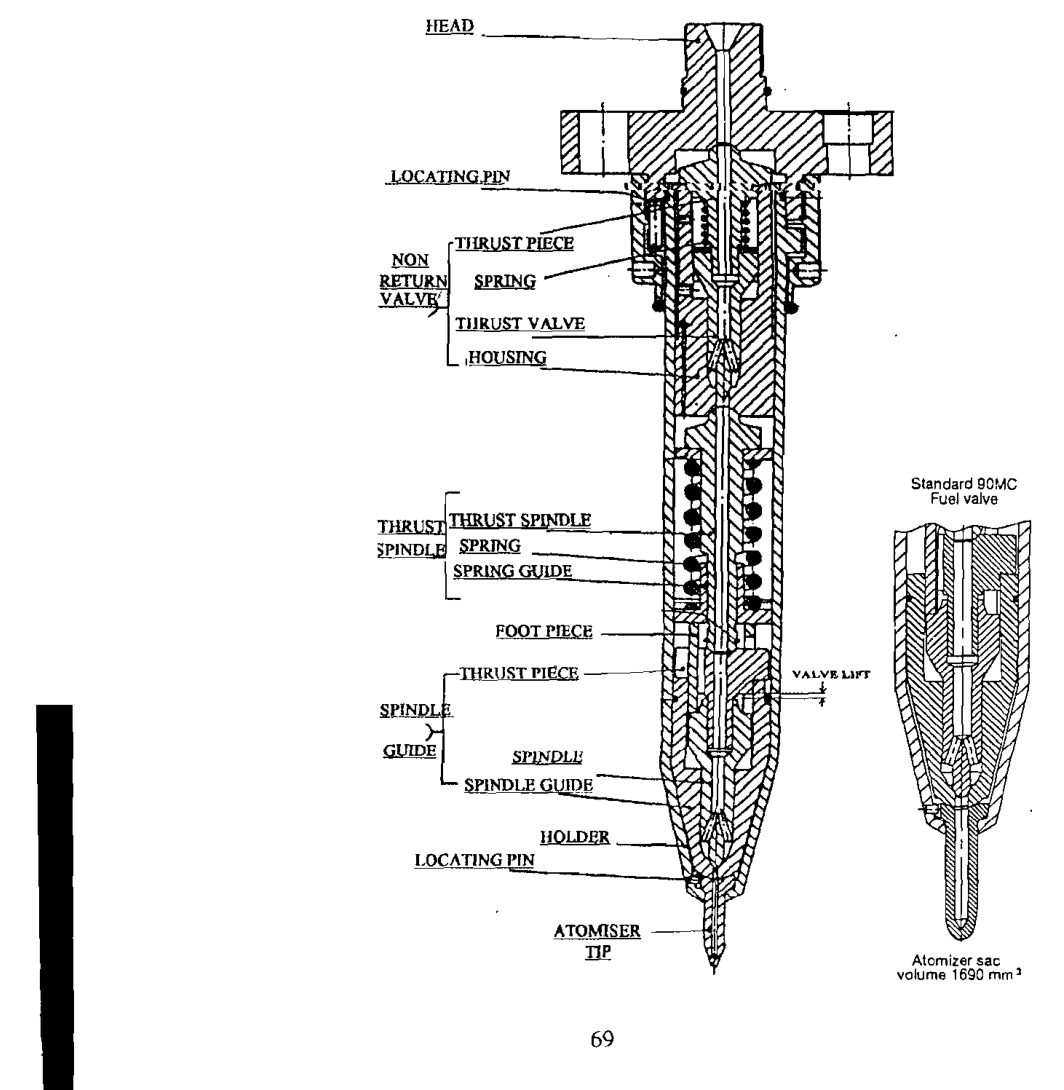
The marine fuel valve is a hydraulically actuated, spring-loaded differential needle valve. Understanding the physics of its opening and closing mechanics is fundamental to troubleshooting injection faults.
The Differential Area Opening Principle (Snap Action)
A fuel injector must open instantly at its designated pressure with zero throttling or dribbling. This rapid opening is achieved through the differential area principle:
Differential Area Equations
Where dguide is the diameter of the precision-lapped needle guide and dseat is the diameter of the conical seat line.
- Valve Closed Phase: The heavy compression spring exerts a downward closing force (Fspring). The needle conical tip rests firmly on the nozzle seat. High-pressure fuel enters the annular pressure chamber surrounding the needle shank, but because the conical seat seals the bottom, fuel pressure acts only on the annular projected area (Alift).
- Opening Threshold (Cracking Pressure): As the fuel pump plunger rises, pressure in the fuel line and nozzle chamber escalates. The needle cracks off its seat the instant: Pcrack × Alift ≥ Fspring
- Snap-Action Opening: The microsecond the needle lifts even 0.01 mm off its seat, high-pressure fuel instantly floods beneath the conical tip into the sac volume. The hydraulic pressure now acts across the entire circular cross-sectional area of the needle guide: Afull = π4 × dguide2 Because Afull > Alift (typically 25% to 35% larger), the upward hydraulic force experiences an instantaneous step-increase. This overpowers the spring force and snaps the needle upward against its upper mechanical stop in less than 0.5 milliseconds, completely preventing partial throttling and seat erosion!
- Crisp Cutoff (Closing): When the fuel pump spills, pressure in the nozzle chamber drops. Because pressure now acts on the larger area Afull, the valve remains open until pressure falls to the closing pressure (Pclose ≈ 0.7 to 0.8 × Pcrack), at which point the spring drives the needle down onto its seat with high kinetic energy, cleanly cutting off spray with zero dribble.
The 1° Seat Differential Angle: 59° vs 60°
To ensure an absolute hermetic seal under pressures exceeding 1,000 bar:
- The conical face of the needle tip is precision-ground to 59° (or 59.5°).
- The internal conical seat of the nozzle body is ground to 60°.
- This 1° angular difference ensures that contact occurs along a microscopic circular line contact at the innermost diameter, rather than across the entire surface area.
- This razor-sharp line contact concentrates the total spring closing force over a minuscule surface area, generating enormous localized contact compressive stress (hundreds of MPa) that crushes any microscopic fuel varnish films and guarantees a gas-tight seal against cylinder combustion pressures!
3. Conventional Sac Nozzle vs MAN B&W Slide-Type Fuel Valve
Environmental emissions regulations (IMO MARPOL Annex VI NOx Tier II/III) prompted a revolution in marine fuel injector design: the transition from conventional sac-volume nozzles to Slide-Type Fuel Valves.
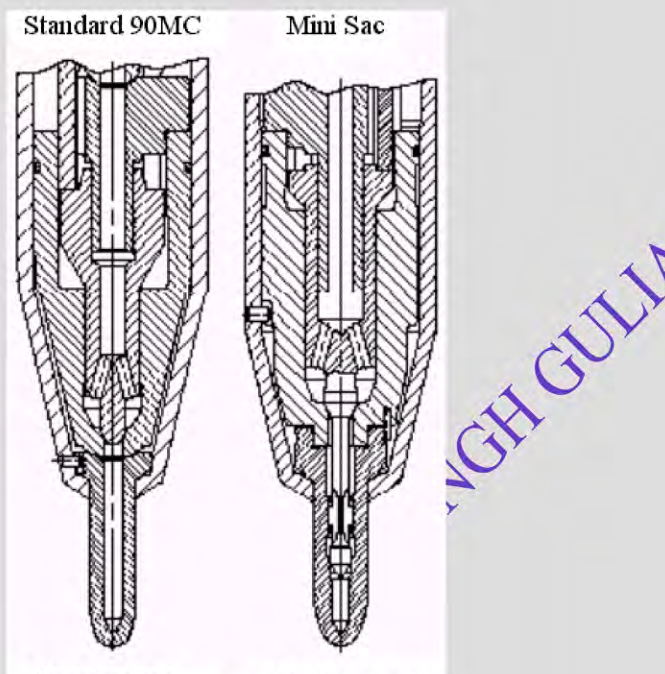
The Conventional Sac Volume Problem
In traditional fuel valves, a small cavity or blind reservoir called the sac volume exists in the nozzle tip beneath the needle seat:
- During injection, fuel flows through the sac and out the spray orifices.
- When the needle closes at the end of injection, a volume of fuel (typically 500 to 1,500 mm3) remains trapped inside the sac, exposed directly to 1,800°C cylinder combustion gases.
- This trapped fuel is at relatively low pressure. It slowly boils, pyrolyzes, and drools out into the combustion chamber as large, un-atomized liquid droplets during the expansion and exhaust strokes.
- Consequences: The drooling fuel produces unburned hydrocarbons (UHC), fine particulate soot (black smoke), carbon trumpet deposits that grow around spray orifices, and localized hot spots that generate thermal NOx.
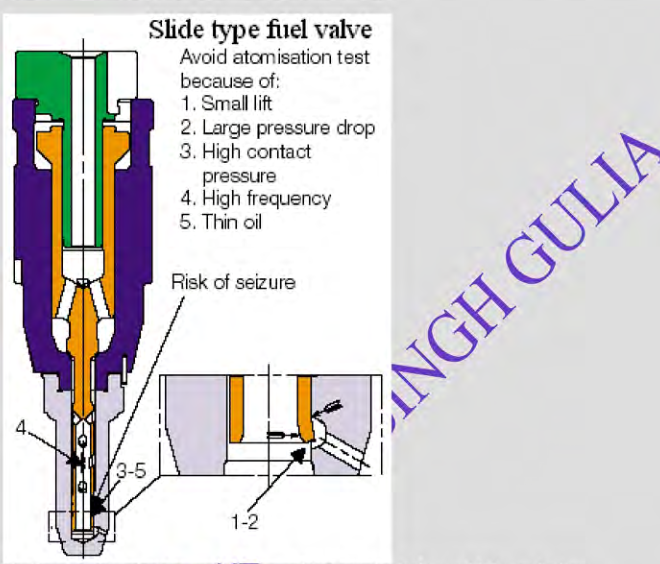
The Slide-Type Fuel Valve Solution
Developed by MAN B&W for modern MC and ME engines, the Slide Valve eliminates the sac volume entirely:
| Design Feature | Conventional Sac Nozzle | MAN B&W Slide-Type Fuel Valve |
|---|---|---|
| Sac Volume | Large blind pocket (500–1,500 mm3). Traps fuel that drools during expansion. | Zero Sac Volume. The slide spindle extends to the absolute bottom of the nozzle bore. |
| Orifice Cutoff Method | Needle seats above the sac; orifices remain open to cylinder gas continuously. | Direct Mechanical Cutoff. The cylindrical slide spindle physically slides over and covers the inlet of every spray orifice the instant the valve closes. |
| Emissions Impact | Baseline UHC and particulate matter emissions; high smoke at low loads. | 50% reduction in unburned hydrocarbons (UHC), 30% reduction in PM soot, and significant NOx reduction. |
| Carbon Trumpet Formation | Severe. Drooling fuel bakes on nozzle tip, forming porous carbon trumpets that distort spray cones. | Virtually Eradicated. Clean, instantaneous cutoff prevents tip wetness and trumpet growth. |
| Nozzle Tip Operating Life | Typically 4,000 to 6,000 running hours before reconditioning. | Extended to 8,000 to 12,000 hours due to cleaner tip temperatures and reduced carbon erosion. |
Warning: Special Workshop Testing Rule for Slide Valves
Marine engineers must note that MAN B&W Slide-Type fuel valves CANNOT be tested on a standard manual hand test pump for atomisation or spray pattern. Because the slide spindle has a very small lift and creates substantial internal throttling at low flow rates, manual pumping produces an asymmetrical, incomplete spray pattern that falsely indicates a defective valve. Slide valves must only be tested for opening pressure and seat tightness on specialized pneumatic/hydraulic test rigs using the manufacturer's designated test adapter.
4. The Seven Workshop Bench Tests on Calibrated Testing Stands
Before any new or overhauled fuel injector is installed into an engine cylinder cover, it must undergo a rigorous, ritualized sequence of seven workshop bench tests on a calibrated fuel valve testing stand.
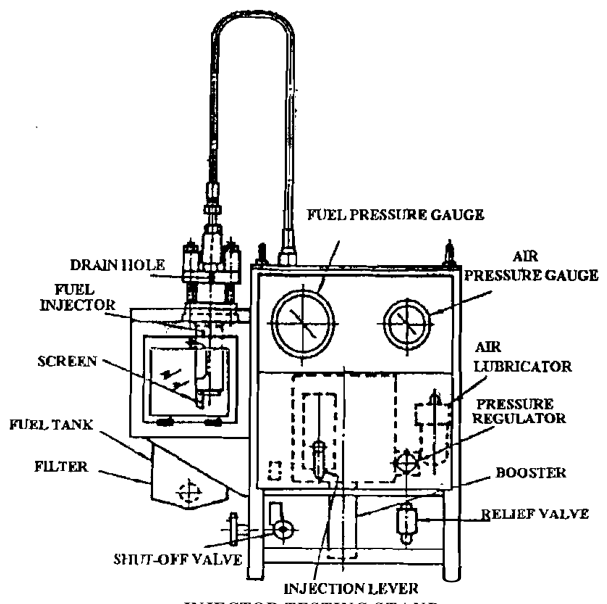
The Seven Bench Tests Protocol
| # | Test Name | Execution Procedure | Pass Criteria & Diagnostic Significance |
|---|---|---|---|
| 1 | Opening (Cracking) Pressure Test | With pressure gauge valve open, pump the hand lever at approximately 1 stroke per second. Observe the exact gauge pressure at which the needle cracks and discharges spray. | Pass: Pressure matches manufacturer's nameplate specification within ±5 bar (e.g., 280–350 bar for two-stroke; 220–250 bar for four-stroke). Adjust via spring compression screw or internal shims. |
| 2 | Spray Pattern & Uniformity Test | Operate pump with rapid, sharp strokes (2–3 strokes/sec). Observe the spray plumes discharging into the transparent acrylic chamber. | Pass: All spray holes fire simultaneously with identical cone angle, equal penetration length, and uniform droplet density. No solid streams, voids, lopsided jets, or deflected plumes. |
| 3 | Atomisation Quality & Chatter Test | Pump the lever rapidly with crisp, short strokes. Listen closely to the acoustic emission from the valve nozzle. | Pass: The injector emits a distinct, sharp, metallic "chatter" or buzzing sound, accompanied by a dry, fog-like mist. Chatter confirms the needle is oscillating freely without sticking, opening and closing crisply. |
| 4 | Orifice Hole Gauge & Wire Check | Clean the nozzle tip and inspect each spray hole using a precision go/no-go pin gauge and magnifying loupe. | Pass: Spray holes are perfectly round without ovality or erosion cratering. A wire probe confirms zero carbon blockage. If hole diameter is enlarged by > 5% to 8% over design diameter, the nozzle is condemned. |
| 5 | Drip / Seat Tightness Test | Slowly raise pressure to 10 to 20 bar below opening pressure (e.g., 280 bar for a 300-bar valve). Close gauge shutoff valve and hold pressure steady for 10 seconds. | Pass: The nozzle tip must remain bone dry. Zero drops, liquid film, or dampness must appear. Any droplet formation indicates a damaged or scored needle seat requiring lapping or renewal. |
| 6 | Back-Leakage (Guide Clearance) Test | Pump pressure to approximately 200 bar, release pump lever, and use a stopwatch to measure the time taken for pressure to drop from 150 bar to 100 bar (fuel weeping past the needle guide into the leak-off return). | Pass: Pressure drop time must fall strictly between 6 and 15 seconds (or maker limit). • < 6 seconds: Excessive guide clearance; fuel slips past needle, reducing injected volume and elevating leak-off. • > 15 seconds: Needle guide is lacquered, tight, or distorted; risk of needle seizure when hot. |
| 7 | Needle Free Movement (Slide Test) | Clean needle and nozzle thoroughly in calibration fluid. Hold the nozzle body at 45° to the horizontal. Pull the needle out by one-third of its length and release it. | Pass: The needle must slide down smoothly and seat completely under its own weight without hesitation or sticking. Rotate 90° and repeat in four orientations. |
Danger: High-Pressure Skin Injection Medical Hazard
Never place bare hands, fingers, or rags near an injector nozzle during testing! High-pressure diesel oil discharging at 300+ bar forms a razor-sharp micro-jet that penetrates human skin instantly without sensation:
- The high-pressure oil dissects subcutaneous tissue, causing catastrophic chemical necrosis, severe gangrene, and toxic bloodstream absorption.
- Victims often report only a minor "pinprick" sensation initially, but within hours, tissue necrosis requires radical surgical debridement or complete limb amputation!
- Safety Rules: Always test injectors inside an enclosed transparent acrylic box with an active exhaust mist filter. Keep hands strictly on the pump lever.
5. Step-by-Step Overhaul, Lapping & Engine Removal Precautions
Overhauling marine fuel injectors requires absolute clinical cleanliness, specialized fixtures, and disciplined mechanical technique. Contamination by a single microscopic grit particle (5 μm) can seize a newly overhauled valve.
Pre-Removal Precautions from the Engine
- Inform the Officer of the Watch (OOW) and obtain Chief Engineer permission before disabling cylinder fuel valves.
- Ensure main engine starting air is shut, turning gear is engaged with safety interlock switch closed, and indicator cocks are fully opened.
- Isolate the cylinder high-pressure fuel pump by pulling its fuel rack to zero and locking the pump cut-out lever.
- Shut fuel oil booster pump supply and return valves to the cylinder manifold; allow fuel temperature to cool to < 60°C to prevent flash fires.
- Loosen the high-pressure pipe union nuts slowly with a backing wrench to vent residual pressure safely into a container before unbolting the pipe.
Disassembly Sequence
- Mount the fuel valve securely in the manufacturer's dedicated bench holding fixture. Never clamp the nozzle body or valve casing directly in a standard bench vise, which will ovalize the precision bore!
- Record the as-found opening pressure on the test stand before dismantling. This baseline data reveals whether the spring has lost tension or if the needle was sticking in service.
- Slacken the spring adjusting screw locknut and completely unscrew the adjusting screw to release all spring tension.
Warning: Spring De-Tensioning Safety Rule
Never unscrew the nozzle holder cap nut while the compression spring is under load! The spring force will strip the cap nut threads and violently launch the nozzle across the workshop, causing severe injury.
- Unscrew the nozzle retaining cap nut using a box wrench and extract the nozzle body, needle, thrust spindle, and spring assembly.
- Immerse all disassembled components in an ultrasonic cleaning tank filled with kerosene or carbon-dissolving solvent for 30 minutes. Use brass wire probes to clear carbon from spray holes—never use steel drills or hardened needles that scratch and enlarge orifices!
Needle & Seat Lapping Procedure
- Inspect the conical seating faces of the needle and nozzle body under a 20× magnifying glass. Light scoring, dullness, or varnish can be reconditioned by precision lapping:
- Use a specialized cast-iron lapping mandrel ground to exactly 60° to recondition the nozzle body seat first. Apply a minute trace of fine diamond lapping paste (600 to 1,000 grit) to the mandrel tip.
- Insert the mandrel into the nozzle body and rotate with a gentle, oscillating, back-and-forth wrist action, lifting the mandrel frequently to redistribute compound. Never spin continuously with an electric drill!
- Clean the seat thoroughly, then apply a smear of 1,000-grit paste to the 59° needle conical face. Insert the needle and oscillate gently against the seat for 30 to 60 seconds to establish a razor-thin, uniform, matte contact ring.
- After lapping, clean every part ultrasonically in clean test oil. Perform the 45° needle slide test to ensure zero lapping paste remains inside the guide.
Reassembly & Installation on Engine
- Reassemble components in reverse order. Lightly lubricate the needle guide with clean calibration oil.
- Torque the nozzle retaining cap nut to the exact manufacturer specification using a calibrated torque wrench (over-tightening distorts the nozzle bore, causing needle seizure).
- Mount on test stand, adjust spring screw to set opening pressure (+5 bar above nominal to account for initial spring bedding), tighten locknut, install sealing cap nut, and execute all seven bench tests.
- Engine Installation: Clean the cylinder cover fuel valve pocket down to bare metal using a brass scraper. Always fit a brand-new annealed copper sealing washer under the nozzle shoulder. Tighten cylinder cover clamping nuts diagonally and evenly in three stages to prevent cocking the valve in its pocket.
6. MEO Class 1 & Class 2 Examination Technical Scenarios & Oral Assessment
Maritime Examiner Oral Assessment Standards
Questions on fuel valve testing, needle lift mechanics, slide valve emissions, and lapping techniques are core requirements in MEO Class 4, Class 2, and Class 1 oral examinations. Surveyors expect exact numerical tolerances and rigorous physical explanations.
Q1: Explain why the conical needle tip of a marine fuel injector is ground to 59° while the nozzle body seat is ground to 60°. What would happen if both were ground to exactly 60°?
Model Engineering Answer:
The 1° angular difference (59° needle vs 60° seat) is a deliberate design feature that creates an exact, narrow line-contact seal at the innermost diameter of the seat.
Reason: Because contact occurs along a razor-thin circular line rather than across a broad cone, the total spring closing force is concentrated over a minuscule surface area, creating enormous contact pressure (hundreds of MPa). This extreme contact pressure crushes any microscopic carbon particles or fuel varnish films, guaranteeing a gas-tight seal against 150-bar combustion gas.
Consequence of Both at 60°: If both needle and seat were ground to identical 60° angles, contact would occur over a broad surface area. The unit contact pressure would be drastically diluted. In addition, manufacturing tolerances would inevitably cause the contact to occur at the outer diameter rather than the inner diameter, allowing high-pressure fuel to seep past the seat and creating constant dribbling, carbon trumpet growth, and premature valve failure.
Q2: Detail the differential area principle that allows a marine fuel injector needle to open with snap action. Why is this snap action essential?
Model Engineering Answer:
Principle: When closed, the needle tip seals the bottom of the pressure chamber. Fuel pressure acts only on the annular area between the needle guide diameter and the conical seat diameter: Alift = π/4 × (dguide2 − dseat2).
When pump pressure rises to the cracking threshold, Pcrack × Alift ≥ Fspring, and the needle lifts slightly off its seat. The instant it lifts, fuel rushes beneath the conical tip, exposing the full guide cross-sectional area (Afull = π/4 × dguide2) to hydraulic pressure.
Because Afull is 25% to 35% larger than Alift, the upward hydraulic lifting force instantly jumps by 25% to 35%, snapping the needle upward against its stop in under 0.5 milliseconds.
Why Essential: Snap-action opening prevents partial throttling. If the valve opened gradually, fuel would seep past the seat at low velocity, producing coarse droplets, seat erosion (wire-drawing), incomplete combustion, and heavy black smoke.
Q3: What is the purpose of the MAN B&W Slide-Type fuel valve, and how does its design eliminate unburned hydrocarbon emissions and carbon trumpets?
Model Engineering Answer:
Purpose: Conventional multi-hole nozzles feature a blind cavity (sac volume) beneath the needle seat that retains 500 to 1,500 mm3 of fuel when the valve closes. In the 1,800°C cylinder environment, this trapped fuel slowly boils and drools into the cylinder during the expansion stroke as large, un-atomized liquid droplets, creating unburned hydrocarbons (UHC), fine soot, NOx emissions, and carbon trumpets around nozzle orifices.
Design Solution: The MAN B&W Slide Valve features an elongated cylindrical spindle that extends down to the absolute bottom of the nozzle bore, achieving zero sac volume.
When the valve closes, the outer surface of the sliding spindle physically slides over and blanks the inlet of every spray orifice directly. This instantaneous mechanical cutoff prevents any residual fuel from drooling into the cylinder. As a result, UHC emissions drop by up to 50%, particulate soot drops by 30%, and carbon trumpet deposits on nozzle tips are virtually eliminated, extending nozzle service intervals to over 8,000–12,000 hours.
Q4: During a workshop bench test, how do you distinguish between a worn needle guide and a leaking needle seat? State the exact tests used.
Model Engineering Answer:
1. Leaking Needle Seat: Diagnosed using the Drip (Seat Tightness) Test:
- Raise pressure to 10 to 20 bar below the opening pressure (e.g., 280 bar for a 300-bar valve) and hold steady for 10 seconds.
- If liquid droplets form or fall from the nozzle tip, or if the tip becomes damp, the needle seat is leaking due to seat erosion, scoring, or poor lapping.
2. Worn Needle Guide: Diagnosed using the Back-Leakage (Pressure Drop) Test:
- Pump pressure to ~200 bar, release the lever, and use a stopwatch to record the time taken for pressure to drop from 150 bar to 100 bar (fuel weeping past the needle guide into the leak-off return pipe).
- Normal time is 6 to 15 seconds. If pressure drops in less than 6 seconds, the diametral clearance between needle and guide exceeds maker limits (normally 3–5 μm). Fuel is excessively bypassing the needle into the leak-off line, reducing the mass of fuel injected into the cylinder. The nozzle and needle assembly must be renewed.
Q5: What are the dangers of high-pressure diesel oil skin injection, and what medical protocol must be followed if an engineer is injured on the test bench?
Model Engineering Answer:
Dangers: Diesel fuel discharging from a nozzle at 300+ bar forms a micro-jet that easily punctures human skin, clothing, and leather gloves. The fuel penetrates deep into subcutaneous tissues, tendon sheaths, and fascial planes. Because the initial puncture wound appears as a tiny, painless pinprick, victims often delay seeking medical care. Within hours, the toxic hydrocarbons cause severe chemical inflammation, vasospasm, acute compartment syndrome, and extensive tissue necrosis (gangrene), frequently necessitating finger, hand, or arm amputation.
Medical Protocol:
- Immediate Medical Emergency: Treat every high-pressure diesel injection as an acute surgical emergency, even if the worker feels zero pain and the skin appears uninjured.
- Never Apply Heat or Tourniquets: Keep the affected limb elevated and immobilized.
- Immediate Hospital Transfer: Transport the casualty immediately to an emergency hospital with an advanced hand/orthopedic surgical team. Inform surgeons immediately that it is a high-pressure hydrocarbon injection injury requiring urgent surgical exploration, decompression, and radical debridement. Provide the Safety Data Sheet (SDS) for the diesel/calibration oil used.
Standards & sources referenced
- MARPOL: International rules to prevent pollution from ships.
- Conventions index
Found a mistake, or something unclear?
Report it in a few seconds — it goes straight to the editors.